During the warehousing and transportation of powdered foods, moisture absorption and caking are practical challenges commonly encountered by manufacturing enterprises. Once products such as milk powder, meal-replacement powders, compound seasonings, and solid beverages become caked and clumped, it directly impacts sub-packaging efficiency and the consumer mixing experience. As anti-caking aids permitted by national standards, food-grade magnesium oxide and food-grade magnesium carbonate can provide a stable and viable formulation solution for powdered foods.
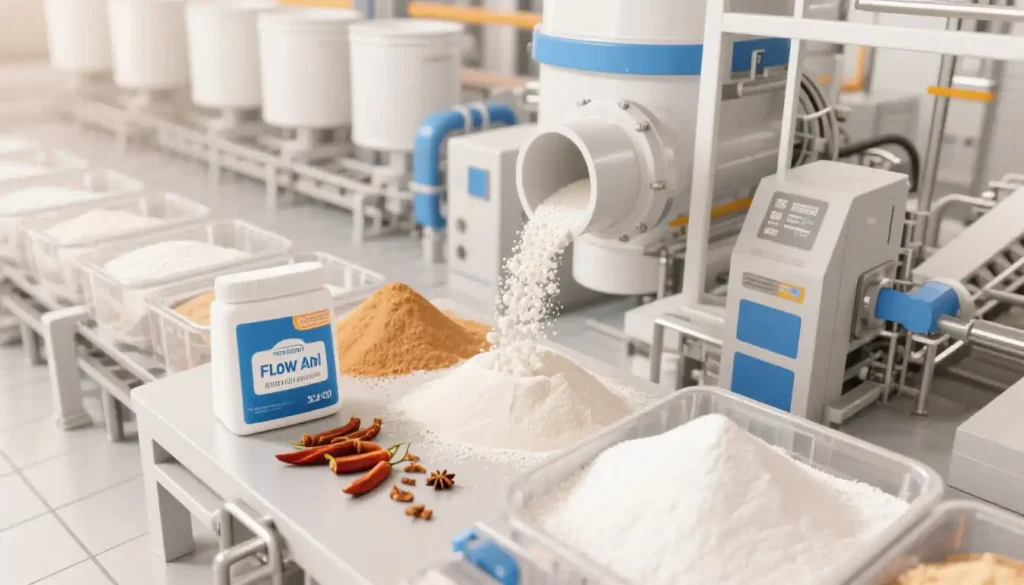
Both exert their anti-caking effects through a physical adsorption and isolation mechanism. Light magnesium carbonate possesses a porous powder structure; when added to a powder system, it coats the surface of the main material particles, adsorbs free water vapor and trace oils within the system, reduces the probability of adhesion between particles, and maintains powder fluidity. Food-grade magnesium oxide also has the ability to adsorb moisture. Heavy magnesium oxide features a higher bulk density and is suitable for powder formulations with higher bulk densities, whereas light magnesium oxide adapts well to fluffy powder products; enterprises can select and match them according to the loose bulk density of their materials.
In actual production, a higher dosage of an anti-caking agent does not necessarily yield better results. According to industry practice, the addition range for most powder products is controlled within 0.1%–0.5%. Excessively high addition amounts can easily cause issues such as an astringent taste and a whitish coloration; therefore, gradient trials must be conducted during the formulation stage in conjunction with the hygroscopic characteristics of the material. Magnesium oxide has a relatively higher elemental magnesium content, enabling simultaneous mineral fortification while delivering anti-caking effects; magnesium carbonate exhibits prominent flow-aiding performance, which benefits feeding and sub-packaging processes on automated production lines and reduces the risk of fill-weight fluctuations.
Raw material compliance is a prerequisite that cannot be overlooked. Enterprises must select food-grade products complying with national standards GB 1886.216 and GB 25587, strictly control indicators such as heavy metals, arsenic, and lead, and prevent industrial-grade magnesium salts from entering the food production chain. Some enterprises compound magnesium oxide and magnesium carbonate together to simultaneously balance anti-caking performance, powder fluidity, and nutritional fortification needs.
As consumer market demands for the quality of powdered foods rise, relying solely on moisture-proof packaging is no longer sufficient to handle complex storage and transportation environments. Rationally selecting magnesium oxide and magnesium carbonate to improve powder physical properties from the formulation source, combined with moisture-proof packaging processes, can reduce caking complaints and strengthen product market competitiveness. When making material selections, in addition to focusing on physicochemical indicators, food enterprises should also verify suppliers’ production qualifications and batch inspection reports to ensure raw material batch-to-batch stability and minimize later-stage formulation fluctuations.